Product Category: Molds
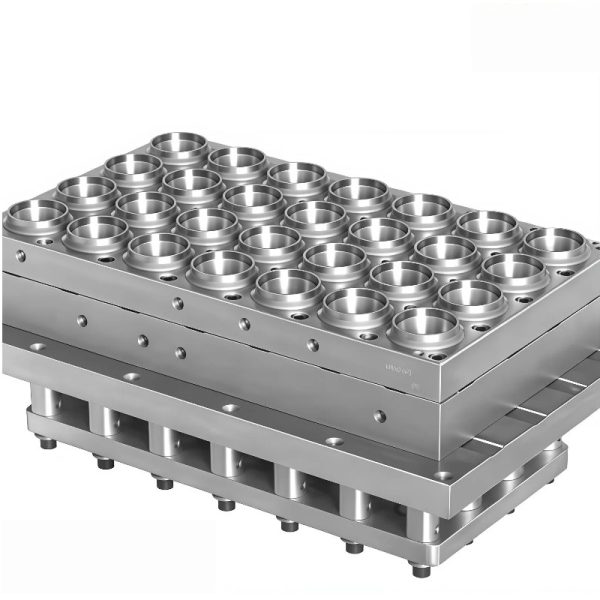
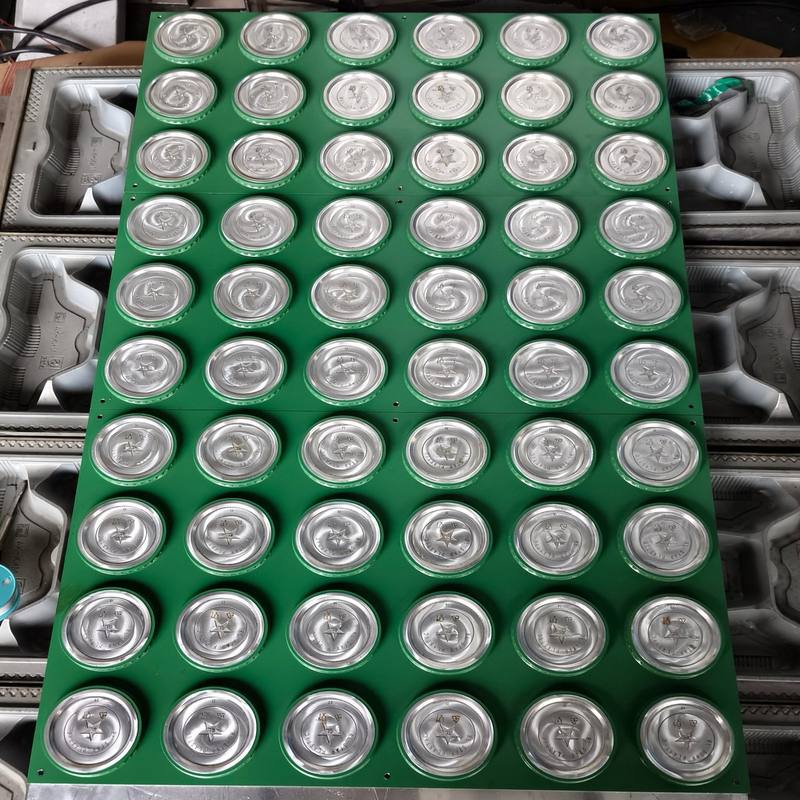
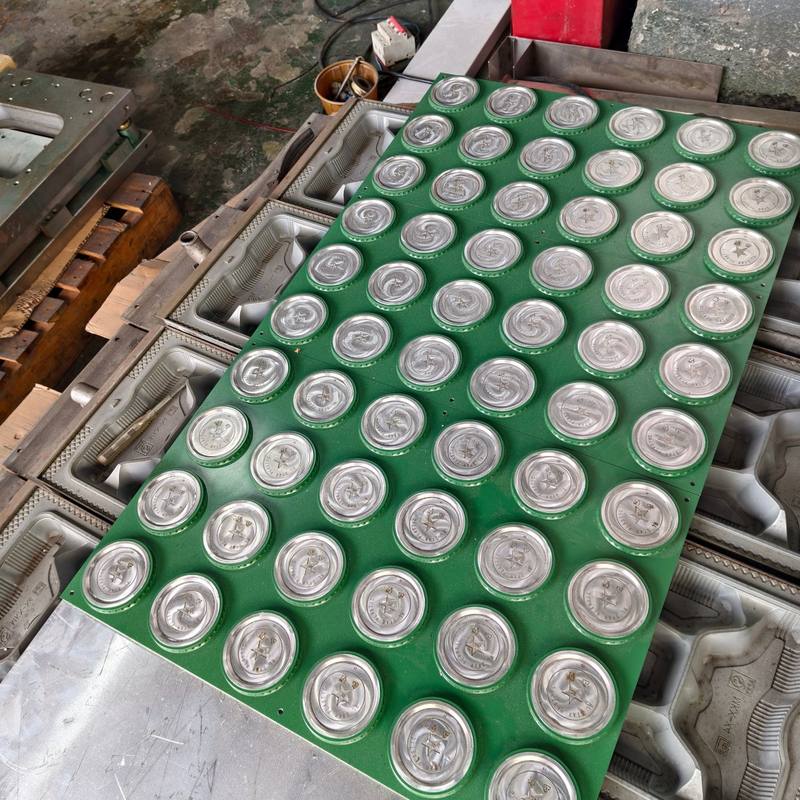
The VihoX-66C-LM represents VihoX’s flagship 66-cavity (6 columns × 11 rows) high-density cup lid thermoforming mold, engineered specifically for high-speed continuous packaging operations. Configured for global standard Ø90 mm and Ø80 mm beverage closures (including milk tea flat lids, bubble tea dome covers, and hot coffee sip lids), this production tooling assembly installs directly onto automatic roll-fed plastic vacuum forming machines and high-speed thermoforming lines. Equipped with high-conductivity 6061-T6 aluminum inserts, micro-porous vacuum evacuation ports, and multi-pass conformal water jackets, the mold delivers sustained outputs exceeding 100,000 to 138,000 pieces per hour with micron-level snap-fit retention reliability.
Complete engineering tolerances, platen interface dimensions, and metallurgical specifications for the VihoX 66-cavity cup lid thermoforming mold:
| Engineering Feature | VihoX-66C-LM Specification | Operational Impact & Tooling Advantage |
|---|---|---|
| Tooling Designation & Type | VihoX-66C-LM / High-Density Multi-Cavity Cup Lid Mold | Massive output tooling engineered for continuous roll-fed vacuum forming machines |
| Impression Grid Layout | 66 Cavities (6 Columns × 11 Rows Symmetrical Grid) | Maximizes sheet utilization across large-platen forming beds (up to 710×1220 mm) |
| Target Lid Diameters | Standard Ø90 mm & Ø80 mm (Customizable Ø75–Ø95 mm) | Fits global milk tea cups, coffee hot drink cups, dessert tubs, and clear cold beverage tumblers |
| Compatible Forming Equipment | VihoX Automatic Roll-Fed Vacuum Formers & Continuous Lines | Direct alignment with chain-rail index pitches and high-tonnage clamping platens |
| Cavity Insert Metallurgy | Certified 6061-T6 Aircraft-Grade Aluminum Alloy | High thermal conductivity ensures instantaneous web chilling and crisp contour definition |
| Rim Locking Geometry | Precision CNC Snap-Fit Undercut Annular Ring | Delivers tight, leak-proof acoustic snap engagement over container rims without splitting |
| Straw Slot & Sip Feature | Integrated Cross-Cut Slit & Star-Embossed Vent Dimples | Pre-engineered straw piercing geometry prevents perimeter tearing during consumer use |
| Evacuation & Venting Network | Perimeter Micro-Porous Vacuum Ports (0.4–0.6 mm) | Rapid air extraction eliminates localized bubbling and ensures flawless optical transparency |
| Internal Thermal Management | Multi-Loop Conformal Cooling Water Manifold | Connects to plant chillers to maintain platen temperature below 15°C during 30 CPM runs |
| Resin Compatibility | PET (Ultra-Clear Cold Lids), PP (Hot Sip Lids), PS, PLA | CNC shrinkage-calibrated to maintain exact rim locking diameter tolerances (±0.05 mm) |
| Production Yield Benchmark | Up to 100,000 to 138,000 Finished Lids / Hour (at 25–35 CPM) | Industrial mass-production scale catering to high-volume commercial beverage brand orders |
| Carrier Base Construction | Heavy-Gauge Precision-Ground Steel & Bakelite Insulation | Prevents thermal transfer into machine platens while maintaining planarity under heavy clamp force |
| Downstream Die Alignment | Precision Dowel Pins for Inline Stacker / Punching Integration | Matches downstream high-speed punching dies and automatic nested lid stacking channels |
| Customization Options | 24 / 36 / 48 / 60 / 66 / 72 Cavity Formats & Custom Brand Logos | Embossed customer brand logos, steam-vent plugs, and dome/flat lid geometry variants |
In the commercial beverage and food service sector, cup lid production is governed entirely by unit economics and production speed. The VihoX-66C-LM utilizes a symmetrical 6-column by 11-row array, compressing 66 individual lid forming impressions onto a single high-strength carrier platen:
The definitive test of a premium cup lid is its acoustic snap and liquid-tight seal over disposable beverage cups. If the locking undercut is machined with even a 0.05 mm error, lids will either pop off during delivery or fit so tightly that retail baristas struggle to apply them.
Every cavity insert in the VihoX-66C-LM features an annular locking undercut profile CNC-engraved to exact micrometer tolerances. The undercut forms a double-contact mechanical seal against matching cup rims produced on VihoX cup making machines, ensuring zero liquid leakage when cups are tipped. Concurrently, the center straw dome integrates a molded star relief structure that allows straw penetration without tearing the outer lid surface.
Continuous thermoforming speeds of 30+ cycles per minute generate tremendous residual heat on the mold face. Overheated tooling causes polymer sticking, slow cycle times, and distorted lid skirts. VihoX manufactures all 66 cavity inserts from certified 6061-T6 aircraft aluminum, chosen for its exceptional thermal dissipation and structural resilience.
Beneath the cavity inserts runs an intricate multi-circuit conformal cooling network. Chilled process water circulated from a dedicated VihoX water chiller at 10°C to 14°C continuously absorbs thermal energy from the forming surface. This rapid quenching solidifies molten PET or PP in roughly 0.5 to 0.7 seconds, allowing instant mechanical part ejection and preventing thermal post-shrinkage distortion.
VihoX tooling engineers calibrate cavity insert dimensions based on the specific volumetric shrinkage curves of your chosen polymer substrate:
Shrinkage factor: 0.2%–0.4%. Produces crystal-clear flat cold lids, dome smoothie covers, and dessert cup closures with sparkling optical transparency.
Shrinkage factor: 1.5%–1.8%. Engineered with elevated steam vents and ergonomic sip spouts for scalding hot tea and coffee takeout containers.
Shrinkage factor: 0.5%–0.6%. Offers high dimensional stiffness and opaque coloration for ice cream tubs and dairy container over-caps.
Shrinkage factor: 0.3%–0.5%. Formulated for biodegradable cold drink lids requiring low mold temperature operation and gentle ejection forces.
While the 66-cavity platen is the benchmark for high-output roll-fed lines, VihoX designs and builds custom cup lid tooling across all commercial output scales:
A multi-cavity lid mold cannot succeed in isolation. It relies on seamless coordination across the entire automated converting line:
The VihoX-66C-LM is engineered primarily for high-demand commercial beverage closures, including Ø90 mm milk tea flat lids with straw slits, Ø90 mm dome lids for whipped cream drinks, and Ø80 mm / Ø90 mm coffee hot-drink sip lids. We can also machine custom embossed brand emblems, secondary straw holes, and teardrop sip-plug tabs directly into the cavity inserts.
By combining a massive 66-impression layout (6 columns × 11 rows) with high-speed cycle kinematics on continuous roll-fed vacuum forming machines. When cycled at a conservative 26 to 32 cycles per minute, the tool generates between 102,960 and 126,720 precision cup lids per hour, providing extreme economies of scale for regional packaging manufacturers.
Each of the 66 circular cavity inserts is CNC-machined from certified 6061-T6 aluminum billets using identical 5-axis toolpaths with tolerances held within ±0.015 mm. The undercut locking bead that snaps onto the cup rim is identical across every station, ensuring that lids from row 1 seal with the exact same tactile retention force as lids from row 11.
Yes, the mechanical mounting fits both materials. However, because PET exhibits minimal shrinkage (0.2%–0.4%) while PP shrinks significantly more upon cooling (1.5%–1.8%), running PP on a PET-calibrated mold will produce loose-fitting lids. VihoX machines dedicated inserts calculated for your target polymer, and we offer quick-interchange insert sets for dual-resin factories.
Optical clarity on transparent beverage lids requires intimate contact between the heated PET sheet and the polished aluminum cavity without trapped air bubbles. The tool features micro-drilled 0.5 mm vacuum relief orifices distributed along the inner rim and logo contours. These evacuate air instantaneously without leaving visible vacuum pin marks on the clear plastic surface.
The 6×11 layout requires an active forming area of approximately 650–710 mm in sheet width and 1100–1220 mm in index length. It mounts directly into standard large-format automatic roll-fed vacuum forming machines and continuous thermoforming lines equipped with mechanical or pneumatic index drives.
Because cup lids are relatively shallow (10 mm to 25 mm deep), overall cycle duration is determined by how rapidly the molten plastic can be chilled below its heat deflection temperature. The VihoX-66C-LM features independent multi-pass chilled water conduits located mere millimeters below each cavity face, slashing cooling dwell to under 0.6 seconds.
Please provide: (1) Target cup rim diameter (Ø75, Ø80, Ø90, or Ø95 mm) or sample mating cups, (2) Desired lid profile (flat cross-cut, high dome, flat sip lid, or flip-tab), (3) Target polymer (PET, PP, PS, or PLA) and sheet thickness, and (4) Your forming machine bed size, index stroke range, and chilled water supply specifications.
Send us your cup lid sample, drawing, or mating cup rim specifications (Ø75 mm to Ø95 mm). Our technical tooling division will prepare a comprehensive cavity array drawing, production yield calculation, and direct manufacturer quotation.
WhatsApp Engineering Hotline (VihoX-66C-LM): +86 147 7547 6896 | Tooling Inquiry: Penny@weihx.com | Main Website: cupmachine1.com
Matched molds and auxiliary equipment — crushers, mixers and recycling units sized to this machine.
See this machine family running in overseas case studies — background, output and on-site photos included.
Request pricing, technical specs or a video machine test — reply within 24 hours.