Product Category: Molds
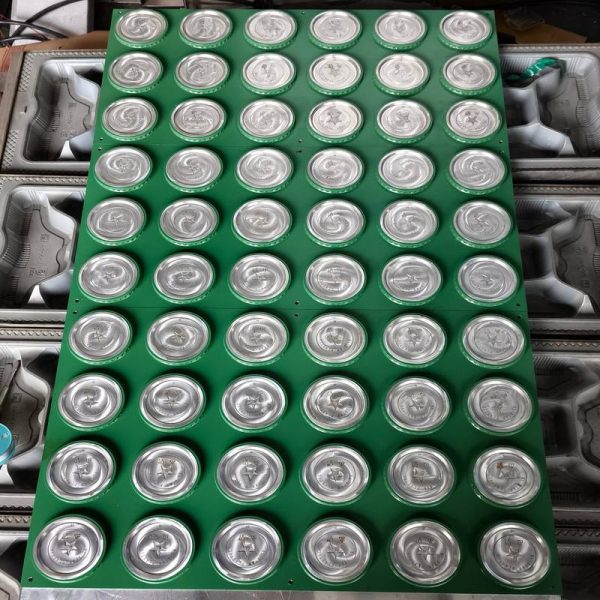
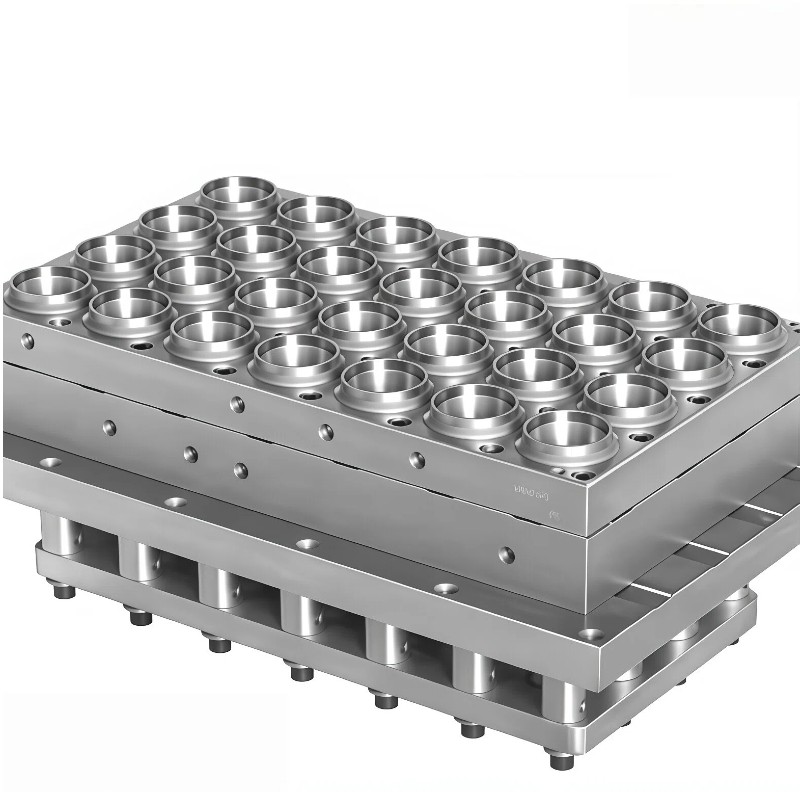
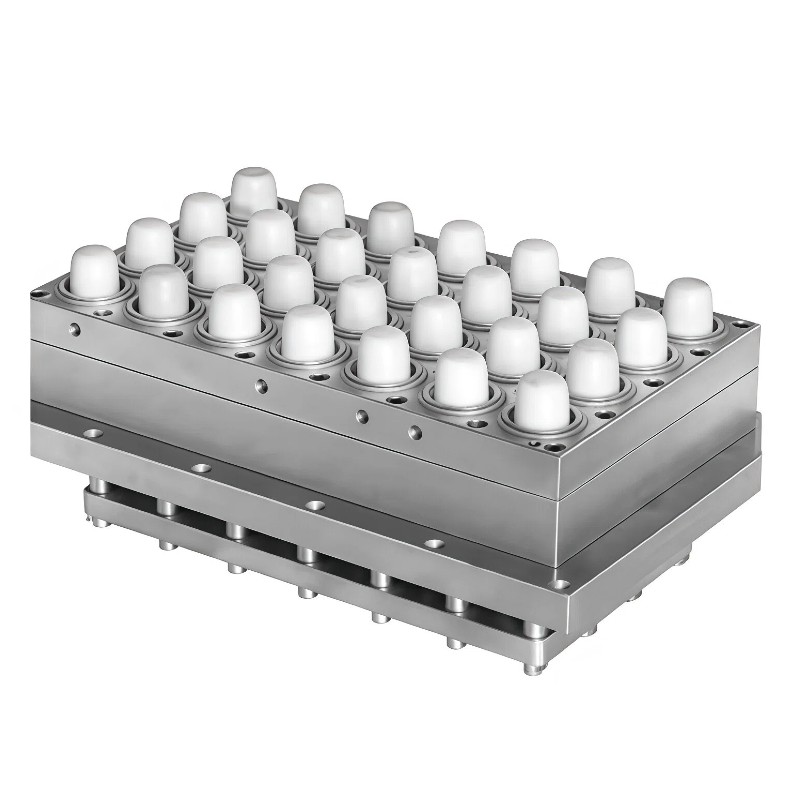
The VihoX-28C-CM represents VihoX’s flagship high-speed thermoforming tooling solution engineered specifically for high-capacity disposable beverage cup manufacturing. Featuring a precision-machined 28-cavity (4 rows × 7 columns) layout optimized for export-standard Ø70 mm water cups, juice cups, and dessert portion containers, this complete mold set pairs directly with our VihoX-750 and VihoX-850 plastic cup making machines. By unifying servo-driven plug assist pre-stretching, high-pressure air forming, integrated in-mold cutting, and high-speed bottom ejection, the tooling achieves sustained production throughputs between 25,000 and 35,000 cups per hour while maintaining micron-level rim dimensional stability.
Review the certified tooling specifications, cavity metallurgy, and mechanical interface parameters for the VihoX 28-cavity in-mold cutting cup mold:
| Engineering Feature | VihoX-28C-CM Specification | Production Impact & Tooling Advantage |
|---|---|---|
| Tooling Designation & Type | VihoX-28C-CM / In-Mold Cutting Cup Mold | Custom engineered for simultaneous forming and rim blanking |
| Standard Cavity Layout | 28 Cavities (4 Rows × 7 Columns) | Maximum cavity density optimized for 750 mm and 850 mm forming widths |
| Target Cup Rim Diameter | Ø70 mm (Standard Export Water / Juice Cup) | Customizable from Ø55 mm up to Ø95 mm for coffee, tea, and dessert cups |
| Recommended Forming Depth | Up to 125 mm (Customizable to 180 mm) | Accommodates 150 ml to 350 ml drinking cups and portion cups |
| Compatible Machine Lines | VihoX-750, VihoX-850 & Equivalent Lines | Direct platen bolting with standardized T-slots and guide pin bushings |
| Cavity Block Metallurgy | 6061-T6 / 7075-T6 Aviation Aluminum Alloy | Ultra-high thermal conductivity for rapid, uniform sheet cooling |
| In-Mold Cutting Ring Material | Cr12MoV / DC53 High-Hardness Alloy Die Steel | Vacuum heat-treated to 60–62 HRC for clean, burr-free rim blanking |
| Plug Assist Pre-Stretch System | Syntactic Foam / POM Engineered Plugs (28 Pcs) | Low thermal conductivity prevents sheet chill; ensures uniform wall thickness |
| Cooling Channel Architecture | Independent Spiral Water Circuit Jackets | Direct connection to VihoX industrial chillers (10–12°C optimal chilled fluid) |
| Polymer Compatibility | PP, PET, PS, PLA & Multi-Layer Barrier Sheets | CNC shrinkage-calibrated for exact dimensional tolerances per resin grade |
| Production Speed Reference | 20 to 32 Cycles / Minute (Line Synchronized) | Yields approx. 25,000 to 35,000 finished cups per hour on high-speed lines |
| Mold Clamping & Alignment | Four-Corner High-Precision Guide Pillars & Bushings | Guarantees micron-level punch-to-die concentricity across millions of strokes |
| Stripper & Ejection System | Servo / Hydraulic Bottom Stripper Plate | Reliable part ejection and seamless hand-off to automatic cup take-out robots |
| Customization Range | 12 / 16 / 20 / 24 / 28 / 32 Cavities Available | Full custom engineering from client 2D/3D part drawings or physical cup samples |
High-volume cup production demands maximum platen utilization without inducing edge deflection or pressure drops across peripheral cavities. The VihoX-28C-CM utilizes a balanced 4-row by 7-column matrix spanning approximately 750 mm × 450 mm of usable mold area. Internal manifold channels balance pneumatic forming pressure (0.6 to 0.8 MPa) across every single impression, ensuring that cavity #1 at the outer corner achieves identical wall thickness and stacking shoulder definition as cavity #14 in the mold center.
Precision ground guide pillars and hardened bronze bushings maintain micro-concentric alignment between the upper plug assist plate and lower cavity block across millions of continuous strokes. Four corner pre-centering blocks lock the tool during final platen closure, completely shielding delicate cutting rings from lateral platen flexure.
Conventional thermoforming workflows that blank cups offline on a secondary trim press suffer from temperature-induced polymer shrinkage, resulting in out-of-round rims, flange cracks, and erratic rim curling. The VihoX-28C-CM solves this through integrated in-mold cutting (forming and punching in the same station):
Deep-draw cups (such as tall drinking cups and beverage glasses with height-to-diameter ratios exceeding 1.2:1) present a severe risk of bottom blowout or excessively thin lower corners if blown purely by air pressure. The upper tool of the VihoX-28C-CM incorporates 28 precision plug assists fabricated from low-thermal-conductivity syntactic foam and engineering POM polymer.
Driven by the thermoformer’s servo plug axis, these plugs advance into the softened sheet just milliseconds prior to compressed air injection. Because the syntactic foam does not chill the polymer sheet upon contact, the material stretches elastically all the way to the bottom cavity radius. When high-pressure air triggers, the sidewall expands with uniform material distribution, saving up to 10% to 15% in sheet raw material consumption while yielding stiffer, more drop-resistant cups.
Cycle time in thermoforming is overwhelmingly governed by heat removal. If a mold cannot evacuate thermal energy rapidly, cups will deform upon stripping or require extended dwell times that drag production speed down. VihoX builds the main cavity block from certified 6061-T6 or 7075-T6 aviation-grade aluminum alloy, delivering thermal conductivity over four times greater than standard mold steels.
Every individual cavity is wrapped with an independent internal spiral water cooling circuit. Chilled water supplied at 10°C to 12°C from a dedicated VihoX industrial water chiller circulates vigorously around the cup walls and base plate, chilling hot PP (melt-forming at 155°C–165°C) or PET (110°C–120°C) down to ejection stability in under 0.8 seconds.
A mold designed for PP cannot simply run PET without dimensional distortion due to stark differences in crystalline shrinkage. VihoX’s in-house tooling division programs custom CNC toolpaths with precise material shrinkage coefficients applied to every critical feature:
Calculated shrinkage: 1.6%–1.8%. Features optimized venting for micro-crystallization and heat-resistant coffee/tea cups.
Calculated shrinkage: 0.2%–0.4%. Delivers glass-like clarity, high rigidity, and tight snap-fit lid groove sealing.
Calculated shrinkage: 0.5%–0.6%. High stiffness, smooth rim curling, and excellent dimensional fidelity for vending cups.
Calculated shrinkage: 0.3%–0.5%. Tailored for bio-degradable eco-cups with low-temperature rapid cooling water jackets.
While the 28-cavity layout represents our most popular export standard for Ø70 mm drinking cups, VihoX provides full-spectrum custom engineering across any container diameter from Ø55 mm to Ø95 mm:
When you source cup molds from a third-party tooling shop, finger-pointing between the machine maker and mold maker inevitably occurs during commissioning. Sourcing tooling directly from VihoX Machinery guarantees unified mechanical, electrical, and pneumatic integration:
The VihoX-28C-CM is optimized for standard export Ø70 mm rim diameter drinking cups (typical volume 200 ml to 300 ml, depth 80 mm to 110 mm). However, our tooling division manufactures custom cavity inserts and complete mold sets ranging from Ø55 mm up to Ø95 mm to suit water cups, bubble tea cups, coffee cups, portion cups, and yogurt containers.
In-mold cutting severs the cup rim inside the forming station at the bottom of the forming stroke using integrated, hardened steel cutting rings. This eliminates thermoforming shrinkage distortion, guarantees 100% concentric cup rims, prevents flange cracking, and removes the need for a separate offline cutting machine, significantly cutting factory footprint and labor costs.
Solid metal plugs quickly conduct heat away from the preheated plastic sheet, causing localized freeze-off and thin cup bottoms. Syntactic foam and engineered POM plugs have extremely low thermal conductivity, allowing the plug to pre-stretch the warm PP or PET sheet deep into the cavity without chilling it, resulting in uniform sidewall and bottom thickness distribution.
The 28-cavity layout (approx. 750 mm × 450 mm mold footprint) is built specifically for our VihoX-750 and VihoX-850 high-speed cup making machines. For smaller forming beds such as the VihoX-660 or VihoX-720, we configure 16-cavity, 18-cavity, or 20-cavity tooling arrays to match platen clamping force and air volume.
Different polymers exhibit vastly different cooling shrinkage rates (PP shrinks 1.6%–1.8%, while PET shrinks only 0.2%–0.4%, and PS shrinks 0.5%–0.6%). We machine cavity blocks with CNC shrinkage factors tailored specifically to your chosen resin grade, ensuring your finished cups hit exact rim stacking dimensions and lid-fit tolerances.
The mold features independent spiral cooling channels across all 28 cavities. We recommend circulating chilled water at 10°C to 12°C with a supply pressure of 0.3 to 0.4 MPa. Connecting this tooling to a VihoX 10HP or 15HP industrial air-cooled water chiller ensures fast heat dissipation and short cycle times without internal mold sweating.
Yes. Every cavity insert, hardened cutting ring, guide bushing, and plug assist is machined to standardized modular drawings with permanent laser-etched serial numbers. Replacement cutting rings and wear components can be ordered and swapped out quickly on-site without re-machining the main base plate.
To receive an engineered mold layout and quotation, please send: (1) Cup sample or 2D/3D technical drawing (specifying top rim diameter, bottom diameter, height, and cup weight in grams), (2) Resin type (PP, PET, PS, or PLA), and (3) Your thermoforming machine model, platen clamping dimensions, and available forming depth.
Send us your plastic cup sample, 2D/3D part drawing, or target dimensions (top diameter × height × weight). Our tooling engineering team will calculate optimal cavity counts, shrinkage factors, cycle times, and machine platen compatibility.
WhatsApp Technical Desk (VihoX-28C-CM): +86 147 7547 6896 | Factory Desk: Penny@weihx.com | Official Portal: cupmachine1.com
Matched molds and auxiliary equipment — crushers, mixers and recycling units sized to this machine.
See this machine family running in overseas case studies — background, output and on-site photos included.
Request pricing, technical specs or a video machine test — reply within 24 hours.