Product Category: PP/PS/PET Sheet Extrusion Lines
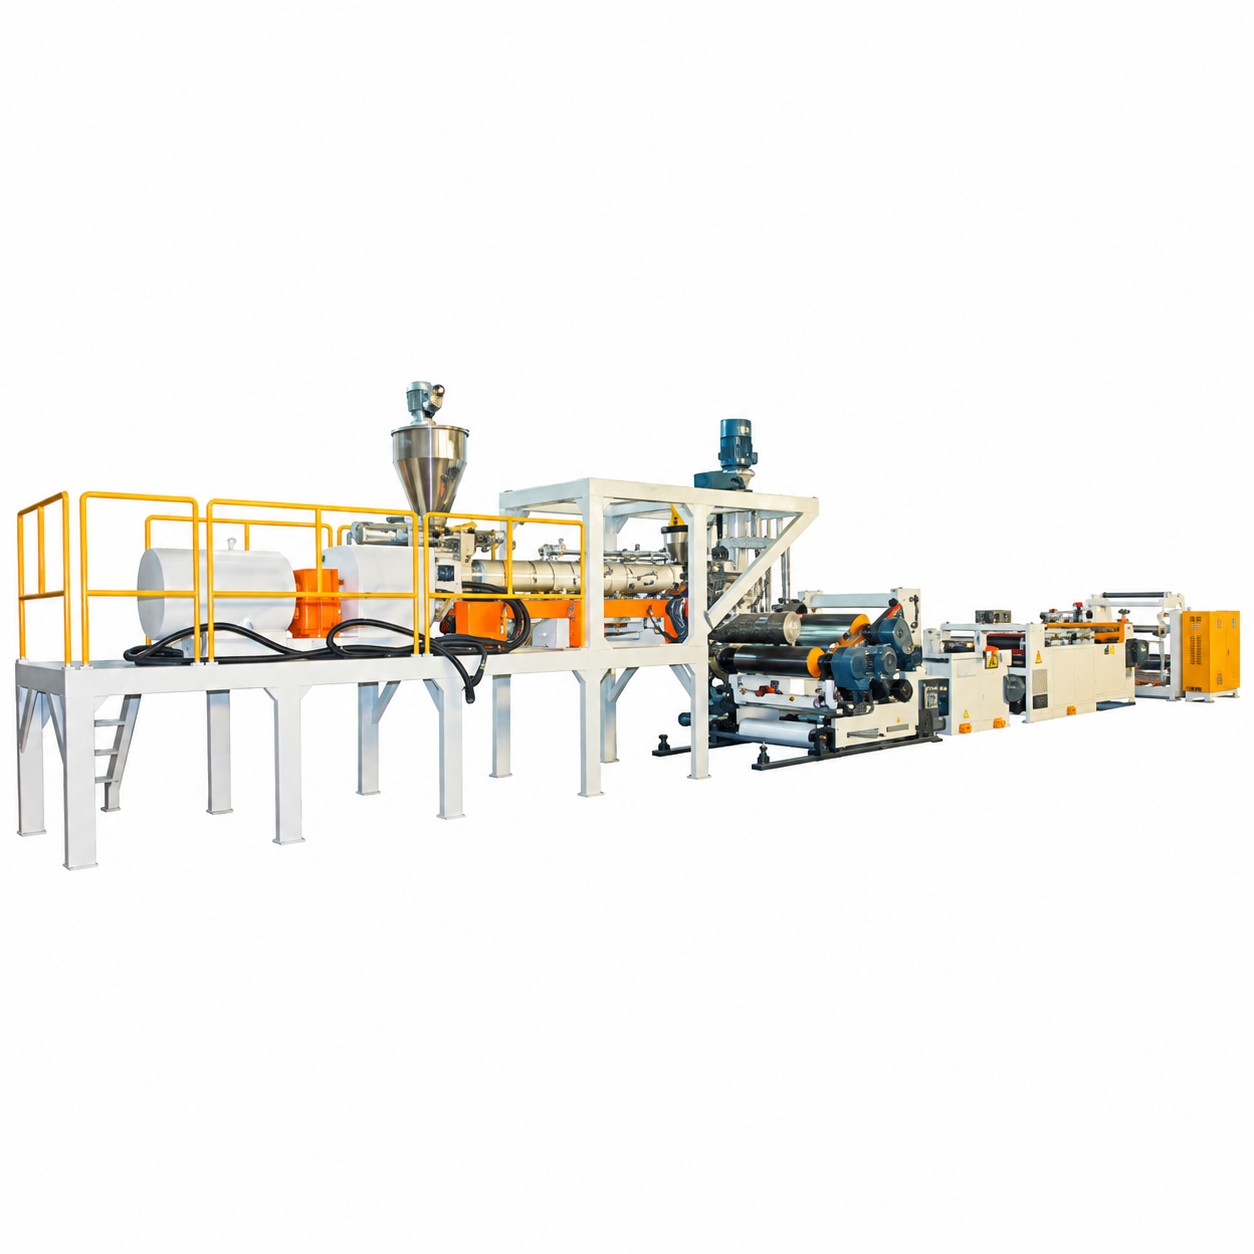
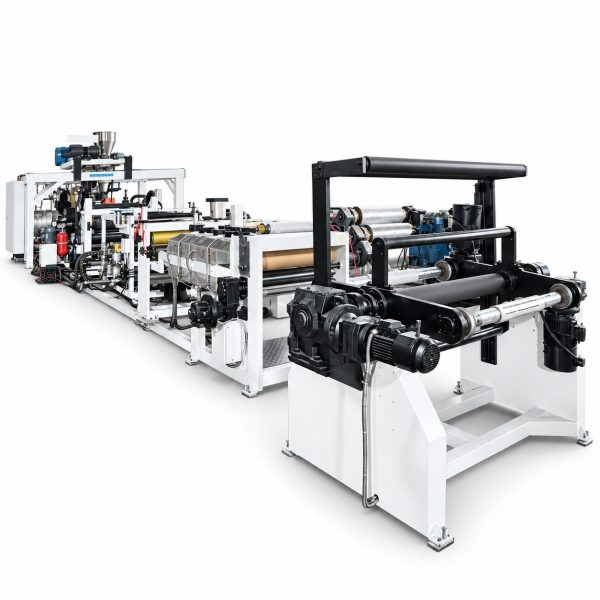
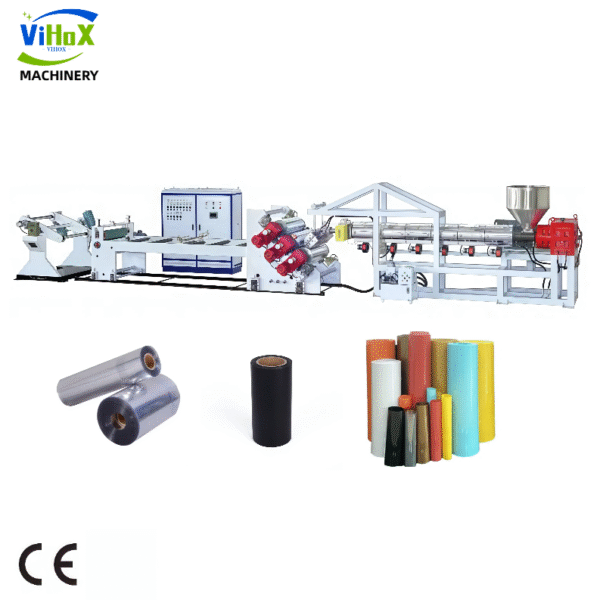
The VihoX 75 PET Parallel Twin-Screw Sheet Extrusion Line is engineered specifically for rigid packaging converters producing clear thermoforming sheets from virgin APET, bottle flakes (RPET), PETG, and bio-based PLA. Built around co-rotating intermeshing twin screws (Φ75 mm × 2) with an extended 44:1 L/D ratio and high-vacuum degassing ports, this extrusion system extracts volatiles and moisture directly from the polymer melt, eliminating costly pre-crystallization and dehumidifying drying hoppers in standard processing workflows.
Delivering a consistent output of 450 to 600 kg/h across finished sheet widths up to 800 mm and calipers between 0.2 mm and 1.5 mm, the line integrates a precision 200CC melt metering pump to suppress pressure surges at the T-die. Downstream sheet calibration is handled by a heavy-duty vertical three-roller polishing stack (Φ350 / 500 / 500 mm) driven by independent servo motors, ensuring optical clarity, zero roller marks, and exceptional thickness uniformity for downstream high-speed cup making and tray thermoforming machines.
Factory trial run: VihoX 75 PET Parallel Twin-Screw Sheet Extrusion Line Running Test
| Specification Item | Engineering Value | Operational Relevance |
|---|---|---|
| Suitable Resins | PET / RPET / PETG / PLA | Wide processing window for food packaging and recycled flakes |
| Screw Diameter & Type | Φ75 mm × 2 (Co-rotating Twin) | Intensive mixing and shear-controlled plasticization |
| Length-to-Diameter Ratio | 44:1 L/D | Extended residence time for multi-stage vacuum devolatilization |
| Sheet Structure | Single Layer (Multi-layer Optional) | Upgradable with co-extrusion feedblock for ABA structures |
| Finished Sheet Width | ≤ 800 mm (Customizable) | Directly matched to VihoX-720 and VihoX-750 cup forming beds |
| Sheet Thickness Range | 0.2 – 1.5 mm | Covers cold drink cups, deli lids, and fruit punnet containers |
| Reference Hourly Output | 450 – 600 kg/h | Stable commercial throughput verified during continuous shifts |
| Main Motor Power | 132 kW | High-torque AC vector drive with closed-loop speed control |
| Total Installed Power | Approx. 310 kW | Includes ceramic heaters, vacuum pumps, and calendar drives |
| Calender Roller Dimensions | Φ350 / 500 / 500 mm | Super-mirror chrome-plated alloy rollers with internal spiral flow |
| T-Die Lip Width | Approx. 1000 mm (Customizable) | Flex-lip coat-hanger design for precise cross-web gauge tuning |
| Production Line Speed | Max. Approx. 15 m/min | Synchronized line tracking from nip rollers to winder station |
| Roller Cooling Architecture | Circulating Water Cooling | Dedicated industrial water chiller recommended for rapid quench |
| Roller Drive Mechanism | Independent Motor Drive | Eliminates gear vibration patterns on thin high-gloss films |
| Melt Metering Pump | 200CC Precision Gear Pump | Absorbs extruder pulsation to maintain ±1% caliper tolerance |
| PET Raw Material Degassing | Strong Vacuum Degassing | Pre-drying avoided depending on moisture levels of pellets/flakes |
| Winding Configuration | Three-Station Winding Unit | Non-stop turret roll turnover with automatic flying cut |
| Electrical Utility Standard | 380V / 50Hz / 3-Phase | Customizable for 220V, 415V, or 480V grid standards |
| Footprint Envelope | Approx. 20–22 × 5 × 3 m | Straight-line layout requiring 4.5 m factory ceiling height |
| Machine Weight | Approx. 25 Metric Tons | Rigid welded steel bed isolating high-speed mechanical vibration |
Traditional PET single-screw extrusion demands prolonged pre-drying at 160°C for 4 to 6 hours to reduce moisture below 50 ppm, consuming immense electrical power and floor space. The VihoX 75 twin-screw design utilizes intermeshing screw blocks that repeatedly divide, smear, and replenish fresh melt surfaces beneath multi-stage vacuum ports operating below -0.098 MPa. Water vapor and residual monomers are instantly evacuated before hydrolysis occurs. As long as incoming flake surface moisture is within reasonable storage thresholds, crystalline pre-drying is safely bypassed, dramatically lowering operational cost per ton of extruded sheet.
For thermoformed beverage cups and bakery clamshells, optical clarity and thickness tolerance dictate high-speed line efficiency. The 3-roller calender features internal spiral cooling channels that distribute chilled fluid evenly across the entire face width, keeping roll surface temperature deviation within ±1°C. Driven by individual gear motors through high-precision universal couplings, each roller can be fine-tuned to compensate for thermal expansion and polymer draw ratios, eliminating surface haze, wave patterns, and stress marks.
Sheet rolls produced by the VihoX 75 extrusion line exhibit outstanding mechanical toughness, excellent deep-draw stretchability, and spotless food-grade hygiene. Key downstream applications include:
Yes. Equipped with dual-piston continuous screen changers and high-torque screw flight profiles, the VihoX 75 handles washed and sorted hot-washed PET flakes directly without requiring re-pelletization.
The melt pump isolates pressure variations originating in the twin-screw melting zones, delivering constant volumetric flow into the die head. This guarantees cross-sheet thickness tolerance within ±0.01 mm.
With clean flake feeds, filter screens typically cycle every 4 to 8 hours. The non-stop hydraulic screen changer permits screen swapping in under 2 seconds without interrupting sheet flow or dropping line pressure.
We recommend an industrial water chiller with a minimum cooling capacity of 20 to 30 HP (approx. 60,000 to 90,000 kcal/h) to maintain roller surfaces between 15°C and 25°C during full-capacity extrusion.
Yes. By setting appropriate lower barrel temperature profiles (180°C–210°C) and gentler screw speed curves via the central PLC touch screen, the line processes PLA without thermal degradation.
The three-station turret winder allows operators to unload completed rolls, index new air shafts, and trigger cross-cutting while extrusion continues at maximum line speed, eliminating production downtime.
A reinforced concrete foundation of 200 mm depth is sufficient. Electrical transformer capacity should be rated at ≥ 400 kVA to support 310 kW installed power with adequate operating headroom.
Yes. VihoX dispatches senior mechanical and electrical engineers globally for complete mechanical positioning, piping, wiring commissioning, and operator training until commercial roll specifications are met.
Contact our technical department directly to test washed flake recipes, verify vacuum port efficiency, or configure inline cup line synchronization.


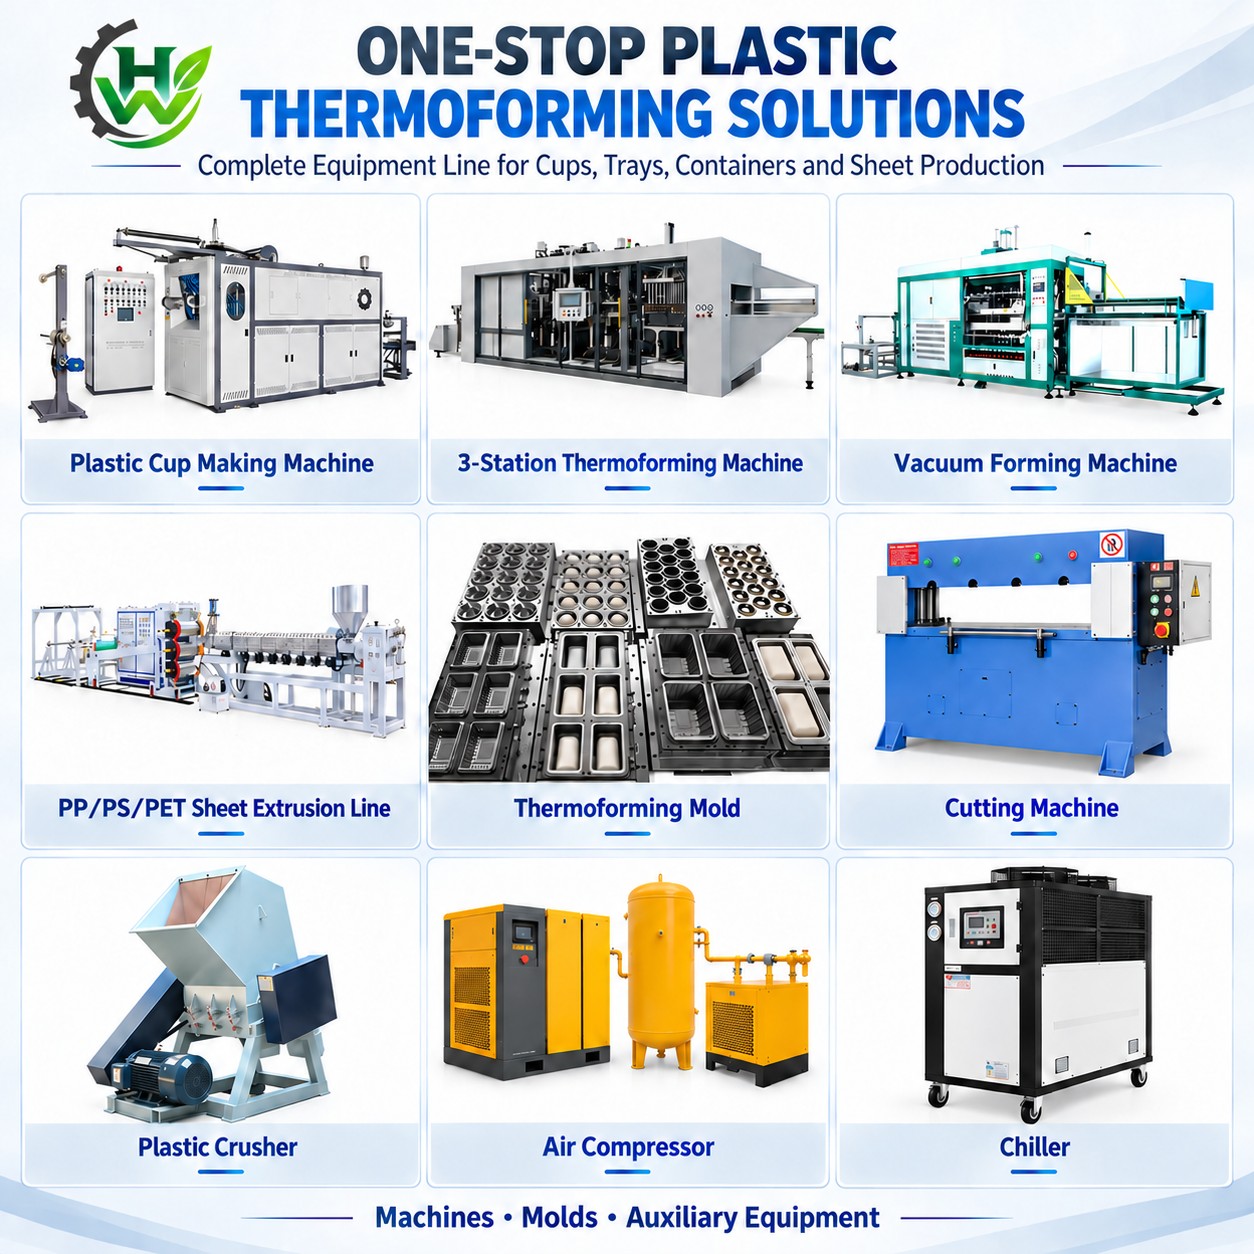
Matched molds and auxiliary equipment — crushers, mixers and recycling units sized to this machine.
See this machine family running in overseas case studies — background, output and on-site photos included.
Request pricing, technical specs or a video machine test — reply within 24 hours.