Built for Plants Running Several Stations at Once
Mid-size forming plants stop thinking in single machines and start thinking in simultaneous demand: a former holding vacuum, a trim press cycling, conveyors and blow-off all drawing from one header. The VihoX 30HP sits in that middle band with 3.64 m³/min of free air from a 22 kW block, matched to equipment drawing roughly 2.0 to 2.8 m³/min in normal operation.
Pressure Stability Under Changing Draw
With a variable-speed permanent-magnet drive, the compressor tracks the header rather than cycling between full load and idle. That matters most where several stations start and stop independently, because the inverter absorbs each step change without the pressure spike and dip that load-banded control produces. Soft starting keeps electrical disturbance to a minimum across the whole plant.
Sizing the Ancillaries for 3.64 m³/min
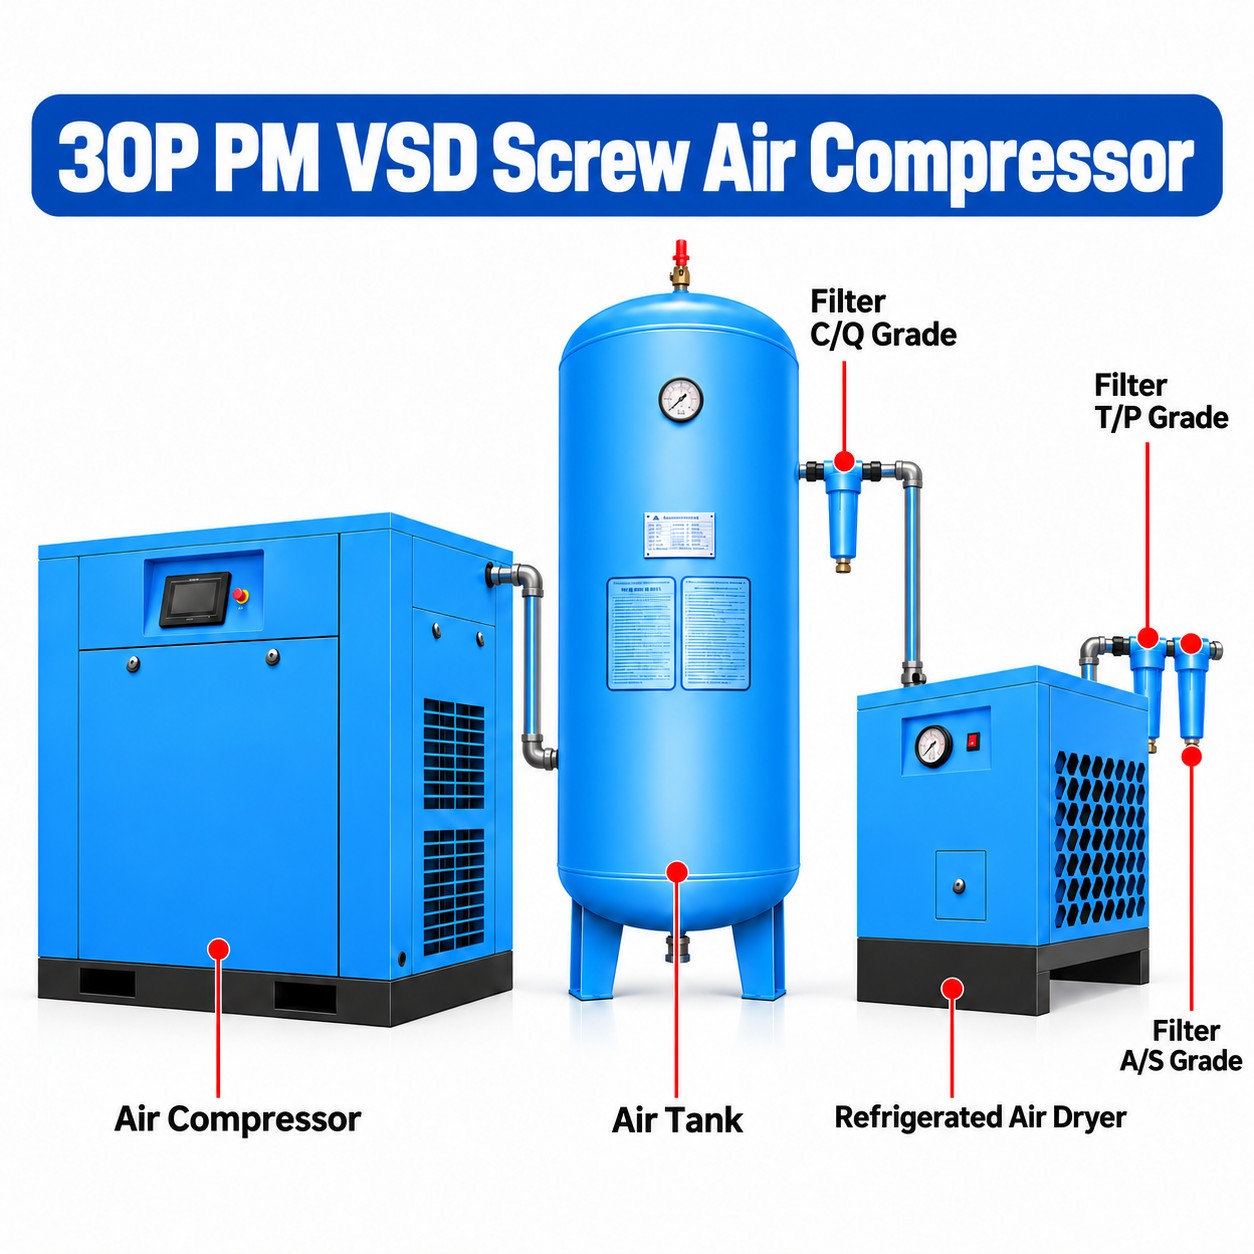
A 1000 litre receiver is the normal companion at this flow, with a refrigerated dryer rated 5.0 m³/min or better so treatment always stays ahead of the compressor. Three-stage filtration protects downstream instruments and blow-off nozzles, and a DN40 main gives enough area for a branched ring without excessive pressure loss.
Air Compressor Specifications — VihoX-30PM
| Rated Value |
VihoX 30HP Setting |
Line-Level Benefit |
| Rated horsepower |
30 HP (30P) |
Tuned for 2.0–2.8 m³/min demand |
| Motor output |
22 kW |
Higher output in the same footprint class |
| Free air delivery at 8 bar |
3.64 m³/min |
Absorbs several forming stations in parallel |
| Usable air after treatment |
2.9 m³/min |
The figure to size tools against |
| Discharge outlet |
G1 to G1¼ |
Two thread options to match pipework |
| Receiver volume |
1000 L |
Smoothes a fast forming cycle |
| Dryer capacity |
≥5.0 m³/min |
Comfortable margin above delivery |
| Distribution pipe |
DN40 |
Sized for a branched ring main |
| Sound pressure |
Approx. 65–73 dB(A) |
Fits a normal production environment |
| Footprint |
Approx. 1300×850×1200 mm |
Compact relative to its air output |
What This Frame Suits Best
The 30HP is aimed at forming equipment drawing about 2.0 to 2.8 m³/min in service. Above that band the compressor spends too much time near full speed and you lose the efficiency advantage of the variable drive, so the next frame up becomes the better engineering choice.
Selection and Installation Questions
Which forming machines suit a 30HP compressor?
Equipment drawing roughly 2.0 to 2.8 m³/min in normal operation, which covers a wide range of mid-size thermoforming machinery.
Why is the outlet offered in two thread sizes?
The frame can be delivered with either G1 or G1¼ so it matches pipework already on site without an adapter.
Is a 1000 litre receiver always the right choice?
It suits most installations. Where demand is unusually spiky, a second buffer vessel can be worth adding.
How much margin does the 5.0 m³/min dryer provide?
Roughly a third above the compressor’s delivery, which keeps dew point steady even in hot weather.
Can two compressors share one dryer?
Yes, provided the dryer’s rated capacity covers the combined delivery with margin to spare.
Does variable speed help when the load is steady?
It does. Holding pressure by modulating speed avoids load and unload cycling, which is where much of the energy loss occurs.
What should be checked before the first start?
Oil level, terminal tightness and that the receiver relief valve is fitted and correctly set for the working pressure.
How often do filter elements need replacing?
Follow the intervals in the manual. A blocked element shows itself as a steadily rising pressure drop across the stage.
Request a 30HP Selection Check
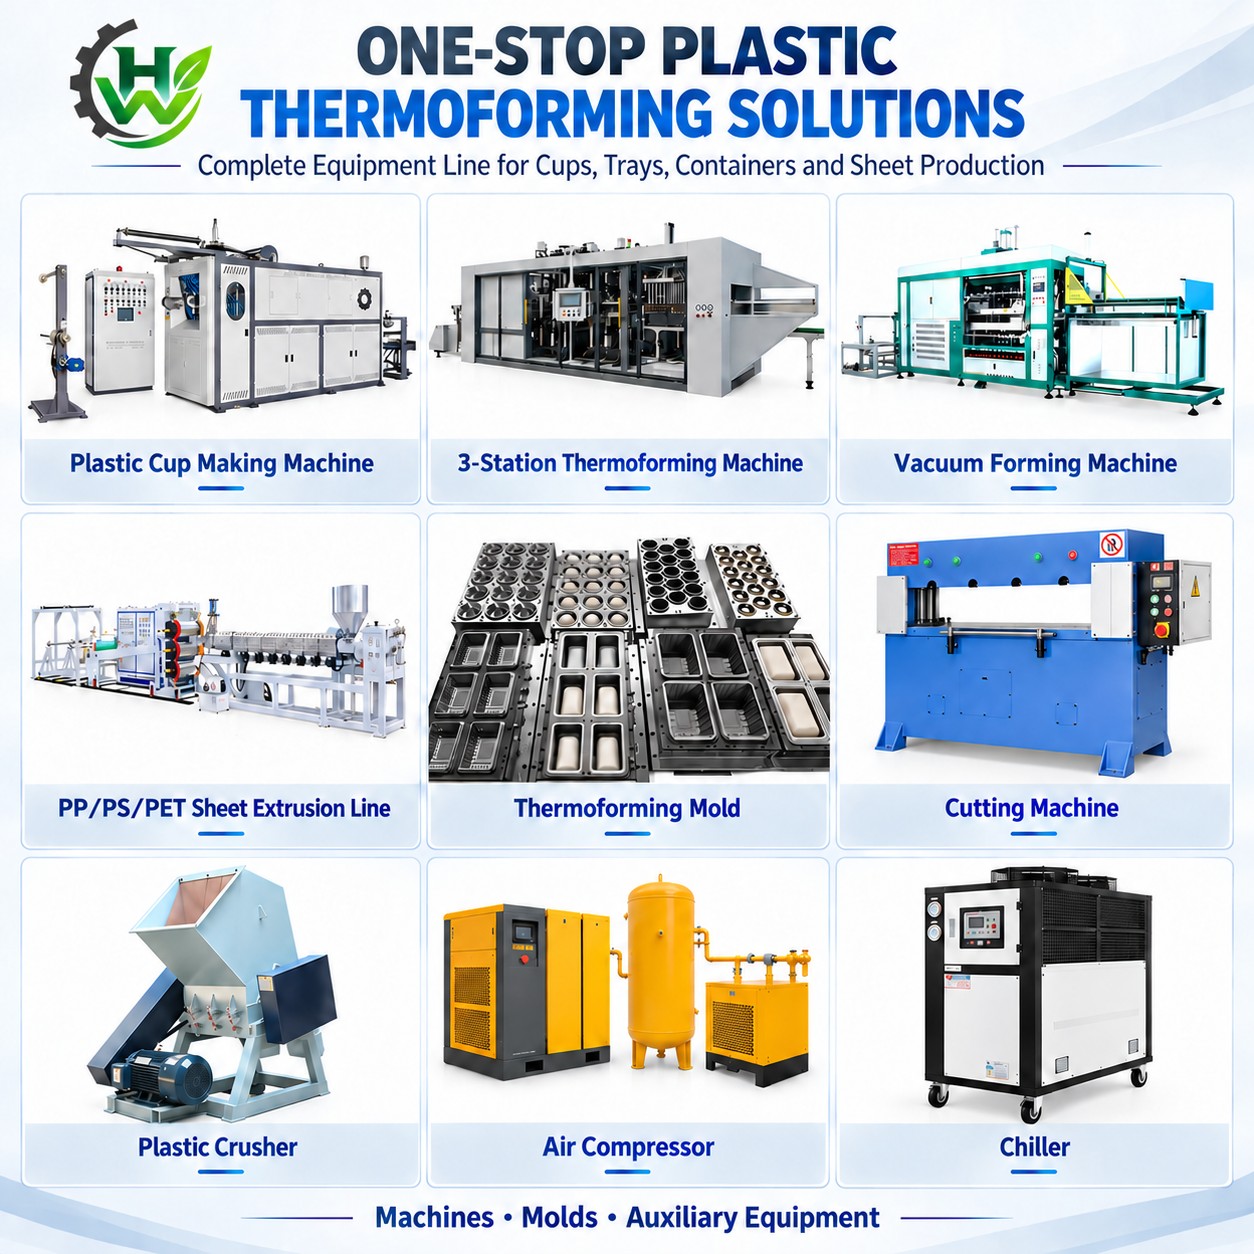
Tell us how many stations run simultaneously, the cycle time of the largest former and your planned pipework route. We will confirm whether 3.64 m³/min holds pressure across the whole header. Useful context: our sheet extrusion lines and auxiliary equipment list the air and cooling support each machine normally needs.
Talk to the factory: +86 147 7547 6896 · VihoX, Shenzhen, China
Supporting Equipment for a 30HP Compressor
Plants at this level normally pair the compressor with an 80 ton counterflow cooling tower and a 10HP air-cooled chiller to cover both bulk rejection and precision cooling. Sheet extrusion lines are frequent air consumers through their trim and conveying systems.