Product Category: PP/PS/PET Sheet Extrusion Lines
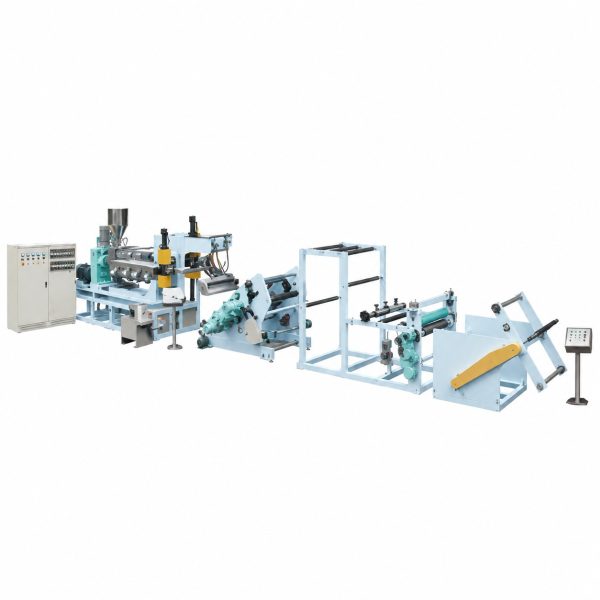
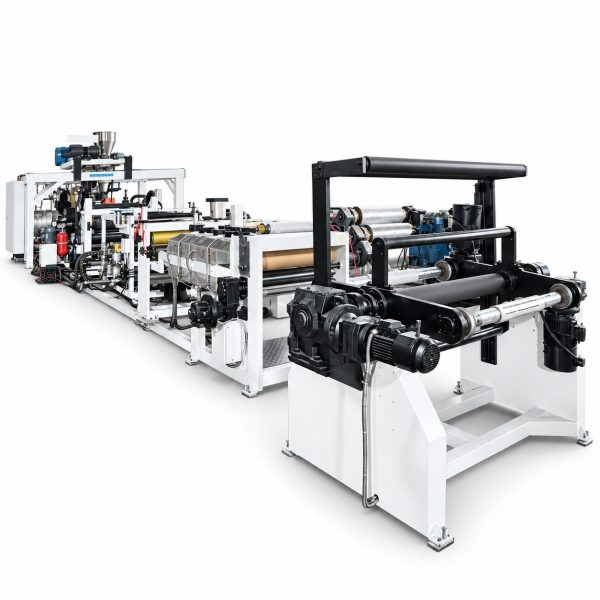
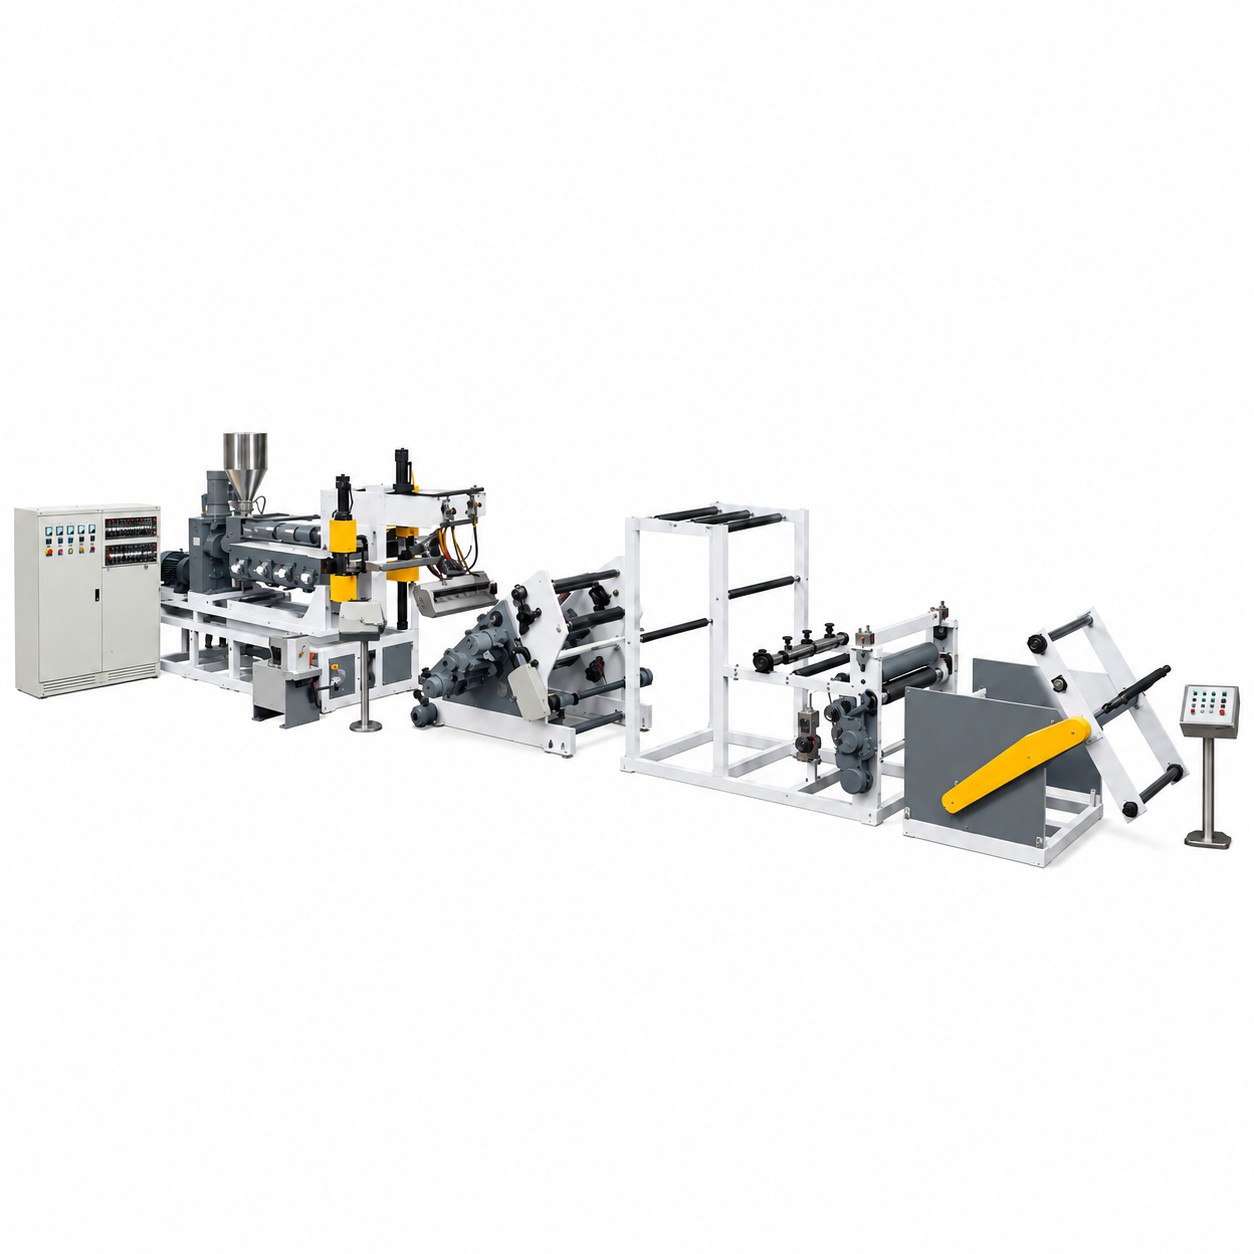
The VihoX 120+65 PP/PS Co-extrusion Sheet Line is our high-capacity multi-layer extrusion platform designed for packaging converters requiring massive commercial throughput combined with sophisticated multi-layer material architecture. Featuring an oversized Φ120 mm primary extruder (90–110 kW motor) and a Φ65 mm auxiliary co-extruder (approx. 45 kW motor), both with a 33:1 L/D ratio, this industrial co-extrusion system reliably produces up to 380 kg/h of multi-layer sheet.
Engineered to fabricate 2–3 layer (AB / ABA) sheet structures across finished widths of 500 to 880 mm and thickness gauges from 0.2 mm to 2.0 mm, the system incorporates a 250CC precision melt gear pump and a 1000 mm coat-hanger die. Downstream cooling is conducted by an enlarged three-roll calender stack (Φ350×1000×1 + Φ450×1000×2) driven by independent AC vector motors, delivering line speeds up to 30 m/min with actual operating electrical consumption of only ~120 kW.
Factory trial run: VihoX 120+65 PP/PS Co-extrusion Sheet Line Running Test
| 380 kg/h Co-Ex Metric | Dual Extruder Specification | Multi-Layer Production Value |
|---|---|---|
| Suitable Resins | PP / PS / HIPS / PE | High-output dual-color sheets and high-regrind ABA core packaging |
| Screw Specifications | Φ120 mm + Φ65 mm Dual Extruders | Large Φ120 mm core extruder enables high regrind volume processing |
| Length-to-Diameter Ratio | Approx. 33:1 L/D | Optimal flight mixing preserving melt strength across both resin streams |
| Sheet Structure / Layers | 2–3 Layers (AB / ABA) | Independent flow adjustment bolts on feedblock for exact layer ratios |
| Finished Sheet Width | 500 – 880 mm | Wide-web compatibility feeding high-speed VihoX cup making lines |
| Sheet Thickness Range | Polypropylene: 0.30–2.00 mm; Polystyrene: 0.20–2.00 mm | Covers ultra-thin portion cups up to heavy-gauge food packaging containers |
| Reference Hourly Output | Approx. 380 kg/h | Massive industrial capacity supplying continuous 24/7 forming shifts |
| Main Motor Power | Main 90–110 kW + Aux ~45 kW | Independent high-torque AC drives with synchronized master PLC tracking |
| Total Installed Power | Approx. 230 kW | Covers multi-zone ceramic heaters, hydraulic packs, and drive vectors |
| Actual Running Power | Approx. 120 kW | Exceptional energy efficiency minimizing operational electricity overhead |
| Calender Roller Dimensions | Φ350×1000×1 + Φ450×1000×2 | High cooling capacity prevents heat buildup during peak 380 kg/h runs |
| T-Die Lip Width | 1000 mm | Streamlined coat-hanger die manifold with thermal differential tuning bolts |
| Production Line Speed | 15 – 30 m/min | High linear web speed matching high-speed automated thermoforming rolls |
| Roller Cooling Architecture | Circulating Water Cooling (Tower/Chiller) | Multi-circuit temperature control units delivering ±1°C roll surface precision |
| Roller Drive Mechanism | Independent Motor Drive | Individual servo motors eliminating mechanical backlash and surface lines |
| Melt Metering Pump | 250CC Precision Gear Pump | High-volume gear pump stabilizing core layer pressure before feedblock |
| Winding Configuration | Dual-Turret Continuous Winder | Surface-center combination winder with pneumatic shaft expansion and automated taper |
| Electrical Utility Standard | 380V / 50Hz / 3-Phase | Engineered for export destinations with custom voltage matching |
| Footprint Envelope | Approx. 12 × 2.0 × 2.5 m | Heavy structural layout providing full accessibility for routine servicing |
| Machine Weight | Approx. 14 Metric Tons | Heavy rigid steel gantry isolating vibration during maximum throughput |
Producing 380 kg of multi-layer polymer sheet per hour requires precise thermal and volumetric control across both extruder barrels. On the VihoX 120+65, the large 120 mm core extruder is coupled with an oversized 250CC precision melt gear pump. This ensures that even when the primary extruder processes 70% crushed skeleton regrind or mineral-filled compounds with fluctuating melt viscosity, the core stream enters the co-extrusion feedblock under completely stabilized pressure, maintaining flawless layer thickness symmetry across the full 880 mm web.
At 380 kg/h, thermal load on the calender rollers is substantial. The VihoX 120+65 features two oversized Φ450 mm rolls combined with a Φ350 mm entry roll, utilizing high-flow internal spiral water circuits connected to dedicated temperature control units. Independent servo drives allow the calender nip, haul-off, and turret winder to synchronize via digital fieldbus, ensuring consistent web tension that prevents roll telescoping, wrinkles, and internal stress during storage.
The high throughput and multi-layer capabilities of the VihoX 120+65 make it the preferred production line for high-volume converters:
The 120+65 delivers approx. 380 kg/h (nearly double the 200 kg/h capacity of the 110+65), driven by a 90–110 kW main motor and a high-volume 250CC melt metering pump.
Yes. By adjusting barrel temperature zones and using appropriate tie-layer masterbatches when needed, the line co-extrudes PP, PE, and HIPS combinations with strong interlaminar bonding.
The 250CC pump isolates extruder surging, ensuring that the heavy core layer flows into the feedblock at constant volumetric rate, maintaining ±0.01 mm cross-web thickness uniformity.
We recommend an industrial water chiller with a nominal capacity of 25 to 35 horsepower (approx. 75,000 to 105,000 kcal/h) ensuring rapid calender roll heat extraction under full-load extrusion.
The feedblock features precision flow restriction bolts for each layer, and the T-die incorporates differential flex-lip bolts to tune both total sheet thickness and individual layer profiles.
Both the 120 and 65 extruders feature non-stop hydraulic slide-plate screen changers, allowing filter screen replacements in 2 seconds without slowing line speed.
A dedicated factory transformer with a rating of ≥ 315 kVA is recommended to support the 230 kW installed power, with typical operating power averaging around 120 kW.
Yes. VihoX dispatches senior mechanical and electrical engineers worldwide for complete positioning, piping, electrical hookup, trial runs, and factory staff training.
Our team will calculate polymer cost reductions when encapsulating internal regrind cores, provide utility schematics, and recommend downstream stackers.
Matched molds and auxiliary equipment — crushers, mixers and recycling units sized to this machine.
See this machine family running in overseas case studies — background, output and on-site photos included.
Request pricing, technical specs or a video machine test — reply within 24 hours.