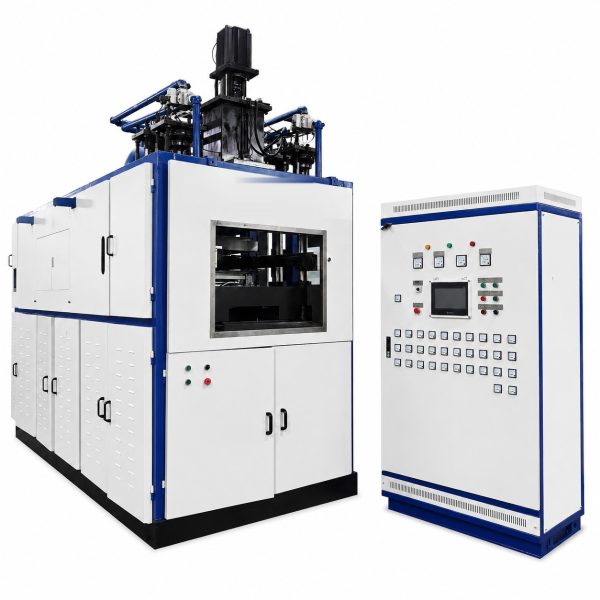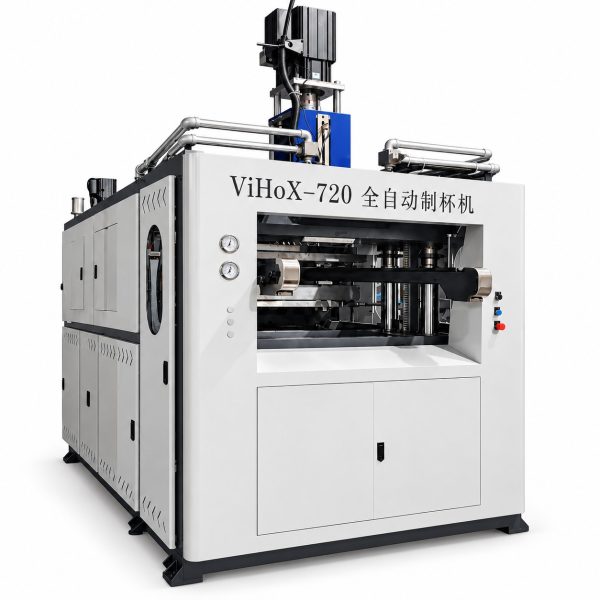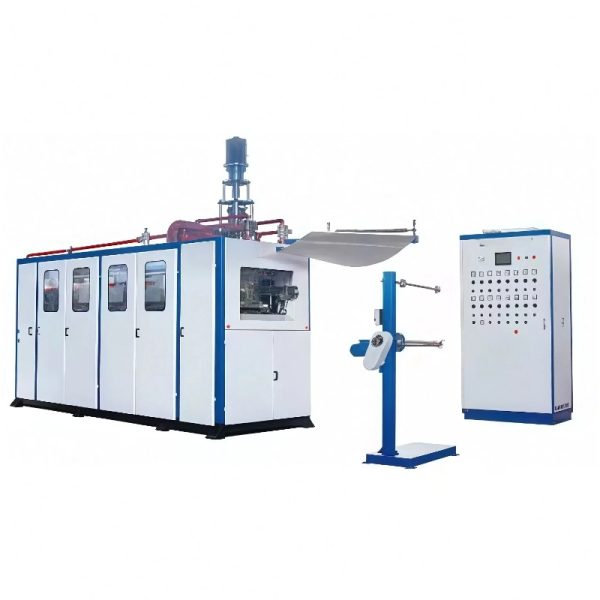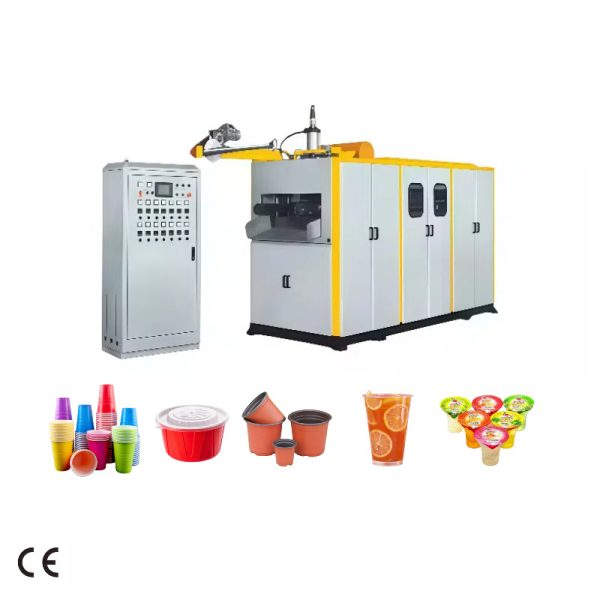
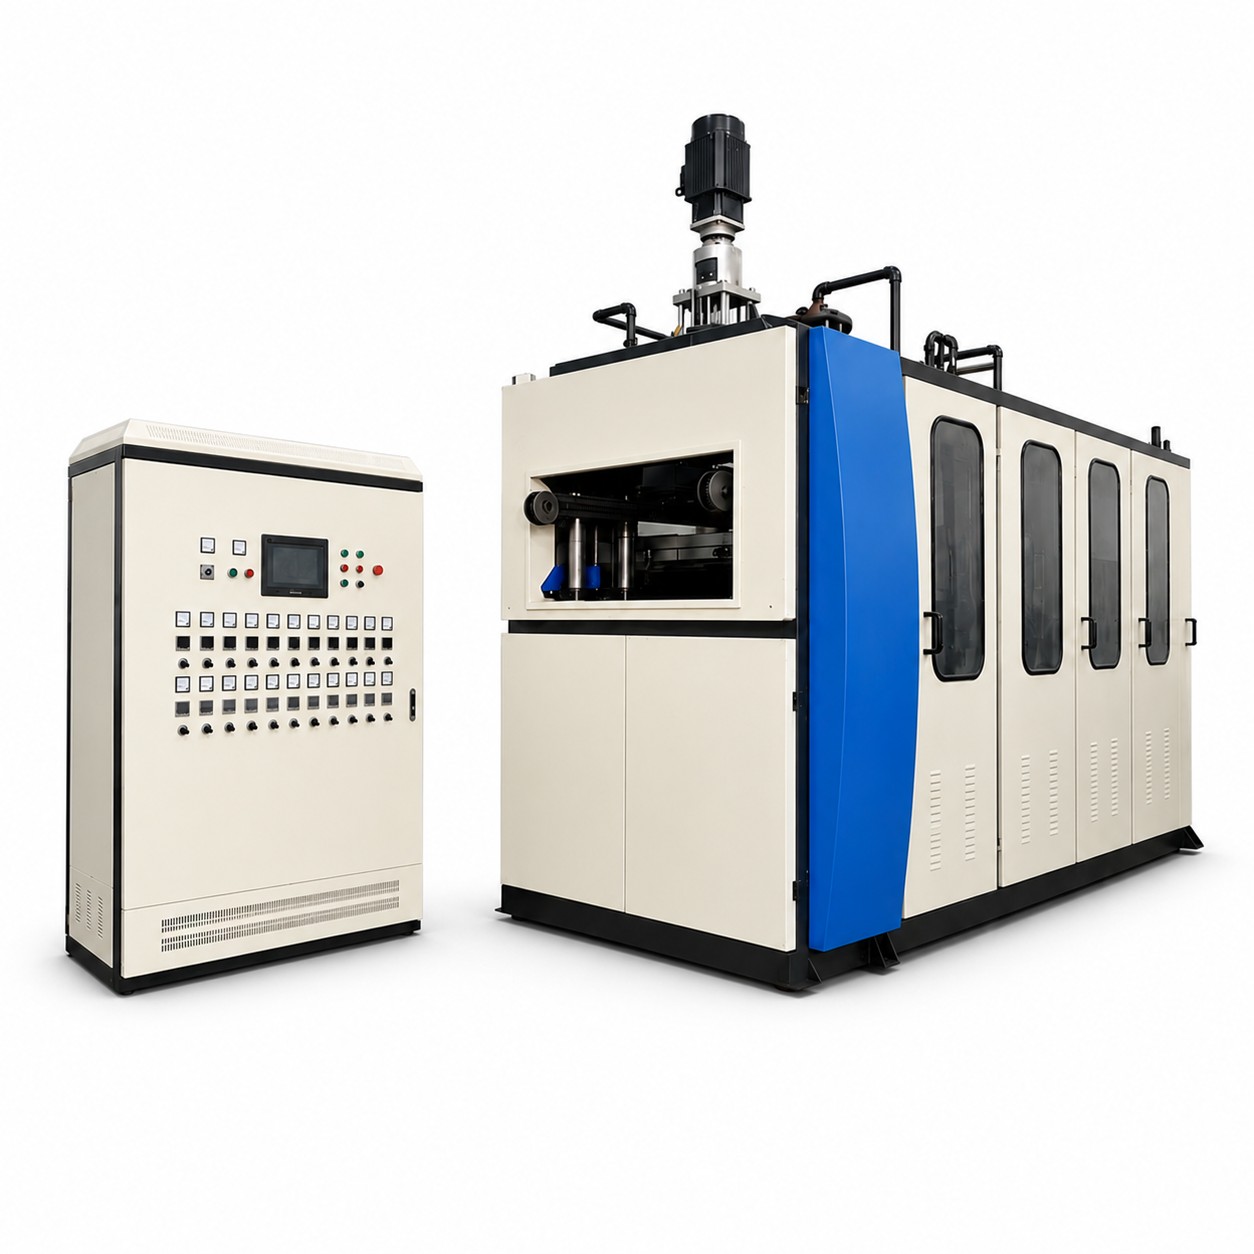
VihoX-750-C Type C full servo automatic plastic cup thermoforming machine: 750×520/750×560 mm forming area, 11 kW stretching servo, 18.5 kW clamping servo, servo sheet feeding, 0.3–3.0 mm sheet, 180/220 mm depth, PP/PS/HIPS/PET/PVC/PLA. Total power and consumption to be confirmed by final servo configuration. Factory tested before shipment.
Product Category: Plastic Cup Making Machines
The VihoX-750-C is a Type C full-servo automatic plastic cup thermoforming machine: a 750 × 520 / 750 × 560 mm forming platform carrying an 11 kW stretching servo, an 18.5 kW clamping servo and a servo-driven sheet feed, so every major motion in the forming sequence runs closed loop.
What a buyer acquires here is behaviour over time. A machine running one shift a week is judged by its initial outlay; a machine running three shifts for years is judged by cycle drift, changeover time and the wear parts demanding attention. The 750-C addresses the second case.
Three drive layouts share one platform, and the dividing line between them is where closed-loop control gives way to cylinder or hydraulic actuation.
| Type | Upper mold drive | Lower mold drive | Sheet feeding | Best for |
|---|---|---|---|---|
| A | Cylinder | Hydraulic | Standard | Straightforward volume work where the product never changes |
| B | Servo | Hydraulic | Standard | Heavy or deep parts where the stretch profile decides quality |
| C (this model) | Servo | Servo (clamping) | Servo | Continuous campaigns that must repeat identically for years |
Full servo changes three things. Cycle consistency improves, because clamping force and stretch position become commanded values rather than pressure-dependent outcomes. Changeovers repeat, because returning to a product means recalling settings rather than rediscovering them. Energy behaviour improves, because the main axes no longer hold force hydraulically all cycle long and the hydraulic scope shrinks with it.
Type C is not automatically right for everyone. Where budget leads, or the product list never changes, the VihoX-750-B or the hydraulic VihoX-750-A covers daily requirements; for small shallow cups the right starting point is a 660 or 720 platform.
| Machine Type | Type C (Upper & Lower Servo + Servo Sheet Feeding) |
| Forming Area | 750 × 520 / 750 × 560 mm |
| Upper Stretching Servo Motor Power | 11 kW |
| Clamping Servo Motor Power | 18.5 kW |
| Max. Sheet Width | 780 mm |
| Sheet Thickness | 0.3–3.0 mm |
| Max. Forming Depth | 180 / 220 mm |
| Speed | 15–35 cycles/min (reference) |
| Air Pressure | 0.6–0.8 MPa |
| Air Consumption | Approx. 3.8 m³/min |
| Water Consumption | Approx. 20 L/min |
| Cooling Recommendation | 5–10 HP Chiller |
| Suitable Material | PP / PS / HIPS / PET / PVC / PLA |
| Power Consumption | 40–80 kWh (reference — to be confirmed by final servo configuration) |
| Total Power (Max.) | 165 kW (to be confirmed by final servo configuration) |
| Power Supply | AC380V / 50Hz / 3 Phase / 4-wire (customizable) |
| Machine Dimension | Approx. L7400 × W2300 × H2700 mm |
| Machine Weight | Approx. 12 T |
| Typical Applications | Water cups, milk tea cups, beverage cups, food containers, bowls, etc. |
How to read these figures
Containers feeding automatic printing, filling or sealing equipment make the clearest case: slight variation at the rim becomes a jam downstream. Dimensions come from the mold, and the envelope is 750 × 520 / 750 × 560 mm with 180 / 220 mm of depth. Small shallow cups belong on a smaller platform, and anything beyond 220 mm depth or 3.0 mm sheet needs an engineering discussion first.
The same six materials apply, but the case for a servo machine varies with each: the narrower the processing window, the more a repeatable cycle is worth.
| Material | Typical cups | Notes |
|---|---|---|
| PP | Hot-drink cups, thick beverage cups, food containers | Forgiving to form; steady clamping helps on long campaigns |
| PS | General food and dessert cups | Predictable behaviour that suits fast, repeated cycles |
| HIPS | Opaque thick-wall cups, bowls, containers | Stiff at higher thickness with solid-colour finishes |
| PET | Clear cold-drink cups, transparent containers | Narrow band between forming and haze; repeatability protects clarity |
| PVC | Industrial and specialised parts | Verify local regulations and end use before selection |
| PLA | Plant-based cups and containers | Very narrow window; controlled heating and a repeatable cycle help |
Sheet roll → servo feeding → heating → servo stretching and forming → cutting → stacking → counting and packing
Feeding, stretching and clamping are commanded together, so the stroke begins at the instant the clamp reaches force, cycle after cycle, with no operator compensating for drift. The gains appear as even wall distribution across a campaign, fewer rejects after a changeover, and a stack that stays level because every cup leaves the tool the same way. A slow stacker still caps output, however precisely the machine draws.
Tooling for a Type C line should be built for its working life rather than a single trial: cavity stability, even cooling channels and a clean cutting edge matter more when the machine runs continuously, because a long campaign multiplies every imperfection. Heat soak is the usual reason a moderate cavity layout outperforms an ambitious one.
Supporting equipment typically covers a 5–10 HP chiller for steady heat removal, a compressor matched to roughly 3.8 m³/min air consumption, cooling water near 20 L/min, plus stacking, counting and packing equipment aligned with the automation level of the line. A stable incoming supply is worth arranging in advance on any machine with substantial servo content.
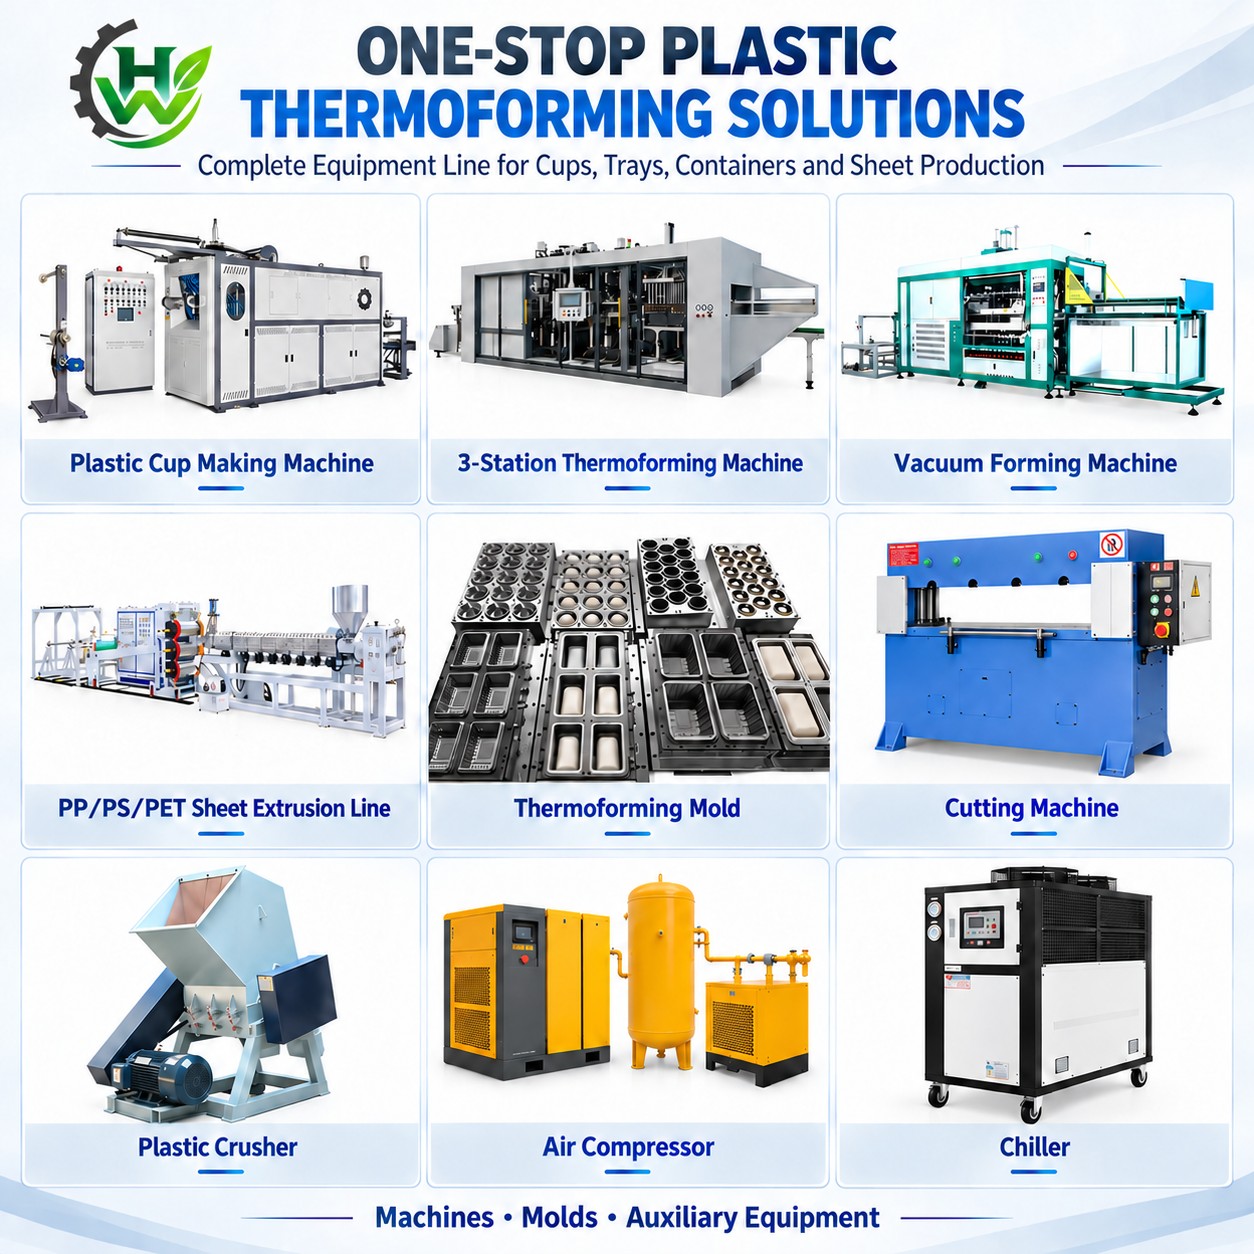
Forming is one station in a longer process, surrounded by sheet supply, molds, cooling, compressed air, stacking, packing and scrap recovery. Factories wanting ownership of sheet width, thickness and formulation — or reuse of their own trim — usually add an extrusion line; those buying dependable roll can start with the machine, the correct mold and a matched auxiliary package.
Related reading: The Plastic Cup Production Line Solution in Full · Auxiliary Equipment for Cup Making · Customer Case Studies · Inside Our Factory · All Cup Making Machines · VihoX-660-A
Machines are assembled, wired and operated under power before dispatch, and the trial is documented: running video, mold trial video, physical samples, cabinet and drive photos, plus drawings, manuals and the spare-parts list. On a servo machine, a trial on your own product and sheet grade is the moment to check forming profile, cutting and stacking together. Factory inspection, a live trial by video, or a third-party inspector before the balance payment are all available.
What does full servo control change in day-to-day production?
Three things: the cycle repeats without drifting; changeovers are quicker because settings are recalled rather than rebuilt; and hydraulic duties on the main axes fall, trimming consumables and checks.
What is the total power and power consumption of the VihoX-750-C?
The machine is quoted as 165 kW maximum power with a 40–80 kWh running reference, but both are to be confirmed by the final servo configuration and are not fixed values. Confirmed ratings are issued with the technical offer.
Should I take the 750-C or stay with the 750-B?
If capital budget leads, or the plant runs one product on a single shift, the 750-B is sufficient and the extra axes would rarely be exercised. The 750-C earns its place on long shifts with frequent changeovers.
Does the machine still depend on hydraulics?
The main forming axes are servo-driven, which reduces the hydraulic scope compared with a Type A or Type B build. The exact content is set by the final configuration.
Which materials can be processed?
PP, PS, HIPS, PET, PVC and PLA sheet from 0.3 mm to 3.0 mm. Material choice affects heating and mold design, so settle it before tooling is ordered.
How is output calculated?
Multiply actual cycles per minute by mold cavities and by 60 for theoretical output, then reduce it for changeover, adjustment, release reliability, stacking interruptions and scrap.
Is full servo worthwhile for a small operation?
Usually not. The C type pays off across long hours and frequent changes, so short batches of one simple cup suit the 750-B or 750-A better.
What information is needed to prepare a quotation?
Cup drawing or sample, top and bottom diameter, height, weight, material, sheet thickness, target capacity, running pattern, factory voltage and country, and whether the scope is one machine or a complete line.
Tell us your cup specification, material, sheet thickness, running pattern and factory voltage. Our engineers will confirm whether the VihoX-750-C is the right drive layout, issue the confirmed power figures for the proposed servo configuration, and quote the matched mold and auxiliary equipment with it.
Matched molds and auxiliary equipment — crushers, mixers and recycling units sized to this machine.
See this machine family running in overseas case studies — background, output and on-site photos included.
Request pricing, technical specs or a video machine test — reply within 24 hours.